How to Choose the Right CNC Screw Machine?
Choosing a Cnc Screw Machine is a production decision, not a catalog exercise. The right choice depends on part geometry, material, tolerance, batch size, and the work your shop already handles. A small turned component may look simple on a drawing. In production, bar-feed stability, tool access, chip control, and changeover time can shape its real cost.
Market growth makes this choice more relevant, but it does not identify the best machine for a particular shop. Grand View Research valued the global CNC machine market at about $101.2 billion in 2023 and projected continued growth through 2030. That figure covers many CNC machine types; it is not a screw-machine sales estimate. The International Federation of Robotics reported 541,302 industrial robots installed worldwide in 2023, a record at the time. These figures point to wider investment in automated production, while leaving a practical question unanswered: will added automation suit your part mix?
The details matter. Compare Swiss-type and conventional turning platforms against the part’s length-to-diameter ratio, required operations, and achievable tolerances. Check spindle capacity, tooling options, programming needs, and support for unattended running. Then compare realistic cycle-time estimates with setup and maintenance demands. A faster spindle is not automatically a faster process. Small parts matter. And machine specifications rarely tell the whole story; a representative trial run can expose issues that a brochure misses. This guide explains how to weigh those factors and choose equipment that fits both today’s workload and likely production changes.
Define Part Requirements and Production Goals
How to Choose the Right CNC Screw Machine?
Define Part Requirements and Production Goals
Start with the part, not the machine. List its material, maximum diameter, overall length, and critical tolerances. Note every feature that affects machining, including cross-holes, grooves, threads, and surface finish. A small threaded fitting may need different tooling and operations than a long pin, even when both use similar stock. Check the drawing carefully. A drawing is not always the whole story; clarify unclear dimensions before requesting a quote.
Then define the production goal. Estimate annual quantity, batch size, and how often the design may change. High volumes can justify a machine setup that takes longer but produces parts quickly. Short runs may favor easier changeovers and simpler tooling. Ask how much setup time, inspection, and secondary work the part requires. A fast cycle is not the entire cost. For example, a part with a milled slot may need an additional operation, affecting delivery time and handling. Share the expected schedule and acceptable scrap rate with the supplier. Real estimates help. Requirements can change after the first batch, so record assumptions and revisit them when actual cycle times and inspection results are available.
Compare CNC Screw Machine Types and Configurations
A CNC screw machine should match the part, not just the production target. Start with diameter, material, tolerance, and part length. A Swiss-type machine feeds bar stock through a guide bushing, supporting slender parts close to the cutting tools. This can reduce deflection on small pins or medical-style components. Short, rigid parts may not need that support.
A fixed-headstock machine often suits wider workpieces and simpler setups. For high-volume, repeat parts, a multi-spindle configuration can machine several pieces at once. That speed has a trade-off: setup and process control become more demanding. More spindles are not automatically better. A modest batch may never repay the added complexity.
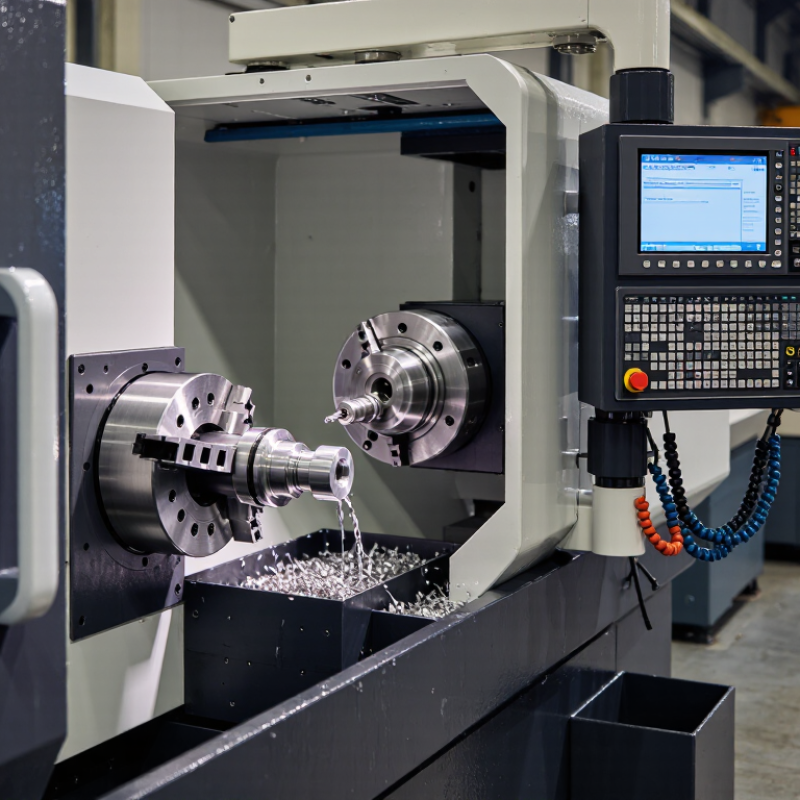
Then compare machine options. A subspindle can finish the back end without manual repositioning. Live tooling can add flats, cross-holes, or milled slots in one cycle. Check bar capacity, available axes, tool positions, and coolant delivery against an actual part drawing. Chip shape matters, too; stringy chips can interrupt production and require adjustment. Ask for a trial using your material and cutting tools. A polished demonstration part may hide difficult changeovers. Leave room for uncertainty: real cycle times can differ from estimates, especially when tolerances tighten or material varies.
How to Choose the Right CNC Screw Machine?
Compare common CNC screw machine types by their typical number of working spindles.
Single-spindle CNC turning centers and Swiss-type machines typically use one main spindle. Multi-spindle automatic screw machines commonly use configurations such as six or eight spindles, allowing multiple operations to run in sequence. Actual configurations vary by machine; consider part size, geometry, tolerances, and production volume when choosing.
Match Machine Capacity, Precision, and Materials to the Job
Choose the machine by its actual part envelope, not its maximum catalog capacity. Check bar diameter, finished-part length, tool positions, and cutoff clearance against the drawing. A 10 mm shaft may look simple, but its tolerance can change the machine choice. ISO 286-2:2010 lists an IT6 tolerance of about 9 micrometres and IT8 of about 22 micrometres for a 10 mm nominal size. Those figures are a useful reference, not a promise of what a machine will hold. Cutting tools, workholding, temperature, and maintenance all affect the result. Small parts matter.
Match spindle torque and machine rigidity to the material. Aluminum, brass, and free-machining steel cut differently; tougher alloys can demand more cutting force and heat control. A bar feeder and spindle may accept the stock, yet the setup can still chatter or wear tools quickly. Ask for a trial cut using the actual material grade, bar size, and tolerance. Inspect several parts, including pieces made after the machine warms up. Heat changes things. Compare cycle time with dimensional stability, not just the fastest demonstration. One weak point in many selection plans is assuming every material listed in a machine’s specifications will run equally well. Check tool clearance, chip evacuation, and available coolant for your part geometry, then confirm the finished surface and dimensions with measurement records.
Evaluate Tooling, Automation, and Total Operating Costs
How to Choose the Right CNC Screw Machine?
Evaluate Tooling, Automation, and Total Operating Costs
A CNC screw machine may look capable on paper, but tooling determines how smoothly it handles real parts. Check the available tool stations, changeover requirements, and compatibility with your current cutters and workholding. Ask how long a representative setup takes, not just how fast a familiar job runs. A sample part tells you more.
Automation can reduce handling, but it adds equipment that needs space, setup, and attention. Consider bar loading, part catching, and in-process inspection against your actual production volume. For short runs, frequent material changes may erase some labor savings. Watch a full cycle, including loading and chip removal. Small delays add up.
Compare total operating costs over a realistic period, such as three to five years. Include purchase price, tooling, maintenance, energy, operator time, and expected downtime. Request service intervals and replacement-part estimates in writing, then compare them with your own production records. One assumption is easy to miss: high spindle utilization does not guarantee profitable output if scrap or changeovers rise. Leave room in the estimate for learning and imperfect scheduling; the numbers rarely stay neat.
| Machine Type | Typical Part and Bar Capacity | Tooling and Setup Considerations | Automation and Labor | Indicative Throughput | Estimated Machine Investment | Estimated Operating Cost per Machine-Hour | Best Fit |
|---|---|---|---|---|---|---|---|
| CNC Swiss-type, single spindle | Small, slender precision parts; commonly about 1–32 mm bar diameter, depending on configuration. | Often needs guide bushings, multiple live tools, and part-specific collets. Setup can be more involved when changing part families. | Bar feeder and parts catcher can support long unattended runs; one operator may tend several machines, depending on workload. | Approximately 100–1,500 parts per hour; strongly dependent on part geometry and cycle time. | About $120,000–$350,000, with bar feeder and auxiliary equipment potentially adding $15,000–$50,000. | About $45–$100, including typical labor allocation, power, tooling, and maintenance; excludes material and financing. | Complex, tight-tolerance small parts, especially when machining features on multiple sides in one cycle. |
| CNC fixed-headstock, single spindle | General turned components; commonly about 3–65 mm bar diameter, depending on machine size. | Uses standard turning tools, collets, and optional live tooling. Tool access and setup are often straightforward for recurring jobs. | Bar feeder and parts catcher are common options. Automation is practical for stable, repeat production. | Approximately 50–600 parts per hour; part size, operations, and cycle time drive output. | About $90,000–$300,000; automation and live-tool options can increase the installed cost. | About $40–$95, including typical labor allocation, power, tooling, and maintenance; excludes material and financing. | Medium-size turned parts, flexible job shops, and work that does not require a sliding headstock. |
| CNC multi-spindle | High-volume turned components; many machines handle bar stock in roughly the 5–32 mm range, subject to configuration. | Multiple stations require coordinated tool packages and careful setup. Tooling costs and changeover planning are significant. | Several operations run simultaneously. Integrated feeding and part handling can deliver high output with limited operator intervention. | Approximately 300–3,000 parts per hour; depends on the number of spindles, part design, and cycle balance. | About $500,000–$1,500,000 or more, depending on spindle count, options, and automation. | About $60–$130, including typical labor allocation, power, tooling, and maintenance; excludes material and financing. | Stable, high-volume production where throughput can justify higher capital and setup costs. |
| Cam-driven multi-spindle | High-volume bar-fed parts; typical capacity varies widely, with many applications in the approximate 5–40 mm range. | Mechanical cams and dedicated tooling require skilled setup. Changes between part families can take longer than on CNC equipment. | Automatic feeding supports continuous production. Operator attention is still needed for setup, tool changes, and quality checks. | Approximately 500–5,000 parts per hour on suitable parts; actual output is application-specific. | About $250,000–$800,000, depending on machine condition, capacity, and included equipment. | About $35–$85, including typical labor allocation, power, tooling, and maintenance; excludes material and financing. | Long, repeat production runs of established part designs where fast cycle times outweigh changeover flexibility. |
| Planning note: All figures are broad, illustrative USD ranges for preliminary comparison, not quotations. Throughput depends on part geometry, material, tolerances, cycle time, and inspection requirements. Operating costs vary by region, shift pattern, labor rates, utilization, and maintenance practice; exclude raw material, facility costs, and financing. Compare total cost per good part across the expected production volume, including tooling, setup time, scrap, automation, and changeovers. | |||||||
Verify Supplier Support and Test the Machine Before Purchase
Before choosing a CNC screw machine, check who will support it after installation. Ask how quickly a technician responds, which spare parts are stocked locally, and what training operators receive. Get these details in writing. A polished sales demonstration cannot show how support works during a real stoppage.
Deloitte and MAPI’s 2019 Smart Factory Study found that 86% of surveyed manufacturing executives expected smart factory solutions to drive competitiveness within five years. That finding is not a service guarantee, but it makes controls, data access, and technical help worth discussing. Ask whether the supplier can troubleshoot alarms remotely and train staff on the machine’s control system. Then run your own part. Use your material, tooling, coolant, and bar stock where applicable. Measure critical features after the machine warms up, and record cycle time, surface finish, and scrap. Run real parts. A tidy demo may hide a weak handoff, and your test may not reflect every shift or material lot. Still, it reveals more than a brochure. Before the trial, agree on acceptance limits and who pays for repeat testing if the machine misses them.